Welcome to the Jodecraft Electroplating FAQ hub—your ultimate resource for mastering the art and science of professional-grade metal finishing. Whether you are an experienced restorer reviving vintage automotive parts, a precision hobbyist crafting custom jewelry, or setting up a full-scale workshop electrolyte line, we know you want answers that are as sharp and reliable as your final plated finish.
Have a specific question you cannot find answered here? Our team is always ready to help you dial in your setup. Dive into the topics below, and let’s elevate your metal finishing to the next level!
Explore our frequently asked questions to discover expert insights on bath maintenance, troubleshooting surface defects like pitting or dullness, selecting the right activators and strikes for difficult substrates, and safely handling and storing your solutions. Everything we formulate and bottle right here in London is designed to give you total control over your results, and this section is built to support you every step of the way.
Navigating the nuances of electrochemistry can sometimes feel like a complex puzzle. From calculating exact bath temperatures and current densities to understanding the precise roles of primary brighteners, levelers, and specialized surfactants, getting the best results takes both quality chemistry and clear guidance. That is why we have compiled this comprehensive knowledge base to cut through the guesswork and give you straight, actionable answers.
Why is surface preparation so important before plating?
Electroplating will not adhere to dirty, greasy, or oxidized metal. Any oil, fingerprint, or surface rust acts as an insulating barrier, leading to peeling, blistering, or patchy coverage. Thorough degreasing followed by acid pickling/activation is essential for a permanent chemical bond.
What basic equipment do I need to start electroplating?
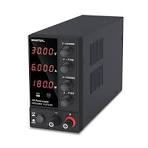
To run a basic benchtop electroplating setup, you need an adjustable DC power supply (0–12V, 0–5A or 0–10A), borosilicate glass or chemical-resistant polypropylene tanks, pure metal anodes (matching your plating bath), titanium wire for suspending parts, deionised water for rinsing, and a digital pH meter or test strips.
Can I use tap water to dilute my plating solutions or rinse parts?
No. Tap water contains minerals, chlorides, and additives like fluoride that contaminate chemistry, cause cloudy deposits, and ruin bath performance. Always use high-purity deionised or distilled water for chemical compounding and rinse stages.
What voltage and current density should I use for tank plating?
Voltage generally ranges between 1.5V and 4.5V DC depending on the chemistry, but electroplating is governed by current density (Amps per square decimetre or Amps per square inch). Always set your power supply using current control based on the surface area of your part rather than relying solely on voltage.
What is the difference between tank plating and brush plating?
Tank plating involves fully immersing the workpiece in a chemical bath surrounded by fixed anodes, making it ideal for uniform coverage on complex parts. Brush plating uses a handheld wand wrapped in an absorbent sleeve soaked in concentrated solution, allowing selective deposition on specific areas without submersing the entire item.
How do I safely raise or lower the pH of my electroplating bath?
To lower pH (make more acidic), add dilute hydrochloric or sulfuric acid drop by drop while stirring continuously. To raise pH (make more alkaline), add a diluted solution of sodium carbonate or potassium carbonate. Always test with a calibrated pH meter after thoroughly mixing.
Why is my plating finish coming out burnt, dark, or rough?
A burnt or rough deposit is almost always caused by excess current density (too many amps for the surface area) or a lack of agitation. Lower your DC power supply amperage, stir the bath gently, or ensure your solution temperature and metal ion concentration are within recommended parameters.
Why is the plated layer peeling, flaking, or blistering off the base metal?
Peeling is caused by inadequate surface preparation or passive oxides on the base metal. Re-clean the part, run it through an acid activation dip (such as dilute citric acid or a bio-pickle) immediately before plating, and ensure you do not touch the bare metal with un-gloved hands.
Why is my plating coverage patchy or non-existent in recessed areas?
Poor coverage in low-current-density areas (recesses and corners) indicates low solution throwing power, improper part orientation, or low voltage/current settings. Rotate your part during plating, adjust anode placement closer to the recessed areas, or check for chemical depletion in the bath.